Identification
Match each tool to its passport, certificate and manufacturer’s marking.
NGB / DRILLING TOOLS
Documented identity, verified condition and tracked service hours. Three requirements for releasing drilling tools to well operations.
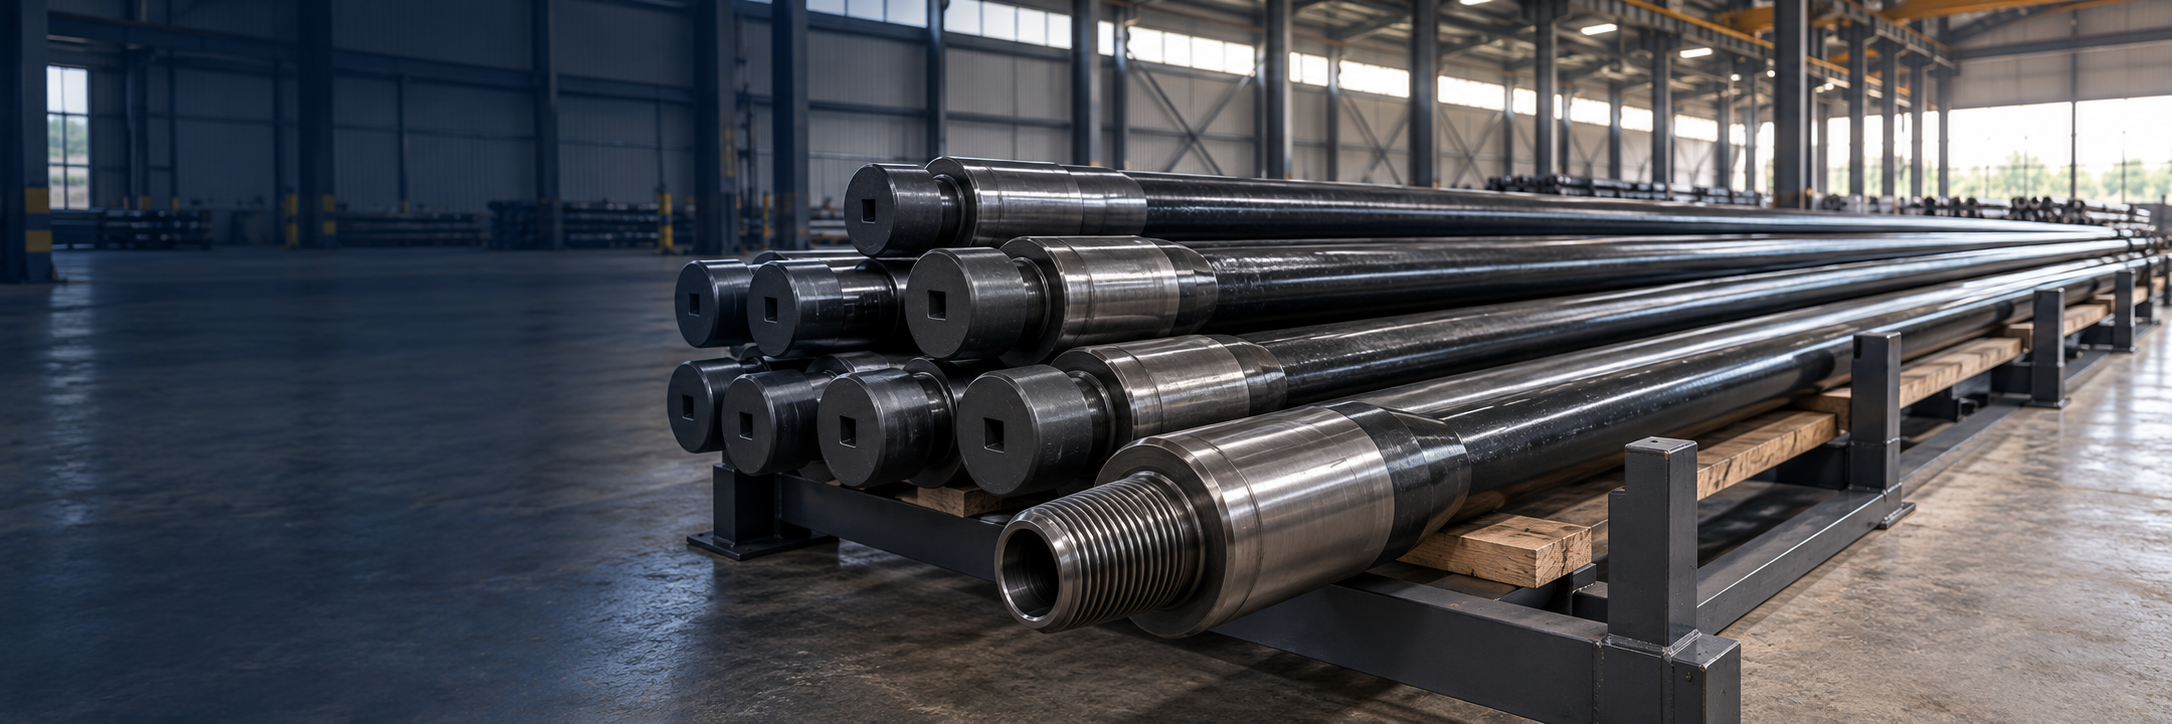
Match each tool to its passport, certificate and manufacturer’s marking.
Inspection, measurement and non-destructive testing before release. Defective tools stay out of service.
Track service hours, inspections, repairs and transfers between wells.
TOOL RANGE AND CONFIGURATION
We select the well-specific tool package by dimensions, condition, connections and design loads. The table distinguishes documented tool specifications from configurations to be agreed in the well programme.
| Tool | Outside diameter | Grade / connection | Application |
|---|---|---|---|
| Drill pipe | 114.3 mm (4½ in) | G105 · NC46 | Primary tool string* |
| Drill pipe (DP) | 127 mm (5 in) | Grade and connection to be agreed | Configuration to the well programme |
| Drill pipe | 73.025 mm (2⅞ in) | S135 · NC31 | Specifications of the documented batch |
| Drill collars | 165.1 / 203.2 / 228.6 mm | Per the relevant passport | Selection to the BHA programme |
| HWDP | 127 mm (5 in) | 1340 + 4137H · NC50 | BHA configuration to the well programme |
| Spiral drill collars / SDC | 247.65 mm (9¾ in) | 4145H · NC70 | BHA configuration to the well programme |
* We select the primary 114.3 mm drill-pipe string according to well design, loads and drilling conditions. Where the project requires it, we provide a 127 mm (5 in) drill-pipe configuration; connection type, grade and quantity are agreed in the well programme.
MANDATORY FOR EVERY NGB PROJECT
This procedure applies to drill pipe, drill collars, heavy-weight drill pipe (HWDP), subs and BHA tools on every NGB project. Stricter manufacturer instructions or well-programme requirements take precedence.
Release is the responsible engineer’s documented decision that an identified tool may be used in the specified well and operating conditions. A manufacturer’s certificate establishes product specifications; release also requires a current condition assessment, compatible connections and a traceable service history.
Tool register + manufacturer documents + current inspection reports + BHA assembly list + service-hour log + written release decision.
Subs require documented material and origin; manufacture from previously used drill collars is not permitted.
API Spec 5DP — Drill PipeAPI Spec 7-1 — Rotary Drill Stem Elements
Manufacturer documents establish product specifications. NGB matches them to each element’s markings and maintains the tool register.
NDT follows an agreed API / DS-1 programme for the tool type. Methods, inspection areas and rejection criteria are set before work begins.
API RP 7G-2 — Inspection and Classification of Used Drill Stem ElementsAPI Spec 7-2 — Threading and Gauging of Rotary Shouldered Connections
The NDT programme follows API RP 7G-2, applicable DS-1 criteria and manufacturer instructions. Inspection before every well and the maximum intervals are mandatory NGB rules.
Keep the BHA drawing and sketches with outside diameter, inside diameter and length. Sub working length must be at least 1.5 times the bore diameter and meet the minimum in the agreed drawing; select bit subs for the specific bit. Spiral integral-blade stabilizers must be 1/8–1/16 inch under nominal, according to size; full-gauge stabilizers are not accepted. At the rig, verify three working Top Drive subs, six lifting caps and six lifting subs for each required drill-collar diameter, at least two safety clamps and two spare drill-collar joints of each size. The assembly list defines additional accessible reserves and required subs.
API Spec 7-1 — Rotary Drill Stem ElementsAPI Spec 7-2 — Threading and Gauging of Rotary Shouldered ConnectionsAPI RP 7G-1 — Drill Stem Performance PropertiesHWDP 127 manufacturer instructions — pages 4–7SDC 247.65 manufacturer instructions — pages 4–5
Selection uses element specifications, connection geometry and permissible loads. The actual tool set must match the agreed BHA drawing.
Every receiving inspection checks both connection ends and protectors; missing protection requires re-inspection.
NOV Grant Prideco 5C — running and handlingHWDP 127 manufacturer instructions — pages 4–7SDC 247.65 manufacturer instructions — pages 4–5
Cleanliness, thread protection and storage follow the specific tool manufacturer’s instructions and NGB receiving procedures.
For drill collars and HWDP, verify make-up at the contractor’s base with a Torque Master-type hydraulic wrench and record actual torque in the passport. Compound requires a quality document and must meet the connection manufacturer’s requirements.
API Spec 7-2 — Threading and Gauging of Rotary Shouldered ConnectionsAPI RP 7G-1 — Drill Stem Performance PropertiesNOV Grant Prideco 5C — running and handlingHWDP 127 manufacturer instructions — pages 4–7SDC 247.65 manufacturer instructions — pages 4–5
Make-up torque and compound are specified for the actual connection. Values for another size or compound are not transferred to the tool.
After every five bit runs, rotate working drill-collar connection positions and check make-up of non-working connections; interchange working and non-working drill-pipe and HWDP connections monthly. Drill-pipe test pressure is 1.5 times maximum working pressure, at least 25 MPa to 4,000 m and 30 MPa below 4,000 m, under a technical programme compatible with the tool set and test equipment ratings. If the required test exceeds those ratings, hold the set until the programme is resolved.
The 600 / 400 / 800-hour limits are set by NGB’s internal procedure. Stricter manufacturer or work-programme requirements take precedence.
After cutting or repairing threads on subs, drill collars or HWDP, repeat NDT before return to service.
API RP 7G-2 — Inspection and Classification of Used Drill Stem ElementsHWDP 127 manufacturer instructions — pages 4–7SDC 247.65 manufacturer instructions — pages 4–5
Additional inspection follows suspected damage, overload, repair or thread cutting, before returning the tool to service.
Replace drill collars according to actual condition and inspection results. The 400-hour limit concerns replacement of subs in the BHA, not automatic disposal of drill collars.
API RP 7G-2 — Inspection and Classification of Used Drill Stem ElementsHWDP 127 manufacturer instructions — pages 4–7SDC 247.65 manufacturer instructions — pages 4–5
Physical segregation, a traceable record and written re-release are mandatory. Rejection criteria are specified for the individual tool.
For drill pipe, BHA subs and drill collars: before each well and at intervals not exceeding 600 hours of drilling and reaming.
Replace subs in the BHA at intervals not exceeding 400 hours. Inspection determines their suitability for further use.
Drill pipe: before work starts and at intervals not exceeding 800 hours of drilling, reaming, hole opening and gauging operations.
These intervals are NGB internal operating limits. A shorter interval required by the manufacturer, the well programme or the actual condition takes precedence. Each inspection, test and replacement is recorded against the identified tool.
TECHNICAL FRAMEWORK
We use the relevant API standards, DS-1 inspection criteria and manufacturer instructions to define product requirements, connection checks and inspection methods. The well programme records the applicable edition and acceptance criteria.
BHA CONFIGURATION
We rent calibrators / stabilizers (KLS) from DENIMEX Ukraine (DENIMEX UKRAINE LLC). Selection follows the well programme. The supplier is responsible for servicing its rented tools.
NGB performs incoming acceptance: match the passport and serial number, review service and inspection reports and operating-hour records, inspect the tool and verify BHA compatibility. Only a documented, suitable tool is released to the well.
Cooperation with DENIMEX UKRAINE LLC for tool rental and servicing is governed by Framework Agreement No. 2611-24 of 26 November 2024. Addendum No. 5 documents the parties’ cooperation.
DOCUMENT LIBRARY
Manufacturer certificates and passport documents for reviewing tool specifications and identity. These documents do not replace a current pre-well inspection report.
Taizhou Elite Drilling Pipe Co., Ltd. Factory documentation; S135, NC31. Original documented batch: 429 pieces, 4130.06 m. Includes factory tests and quality checks.
Download PDF7 p. · 2.15 MBTaizhou Elite Drilling Pipe Co., Ltd. Factory documentation; G105, NC46. Original documented batch: 484 pieces, 4618.45 m. Includes factory tests and quality checks.
Download PDF6 p. · 1.70 MBTaizhou Elite Drilling Pipe Co., Ltd. Factory documentation; G105, NC46. Original documented batch: 484 pieces, 4618.45 m. Copy for the same batch.
Download PDF3 p. · 1.68 MBTaizhou Elite Drilling Pipe Co., Ltd. Factory documentation; S135, NC31. Original documented batch: 429 pieces, 4130.06 m. Copy for the same batch.
Download PDF3 p. · 1.68 MBJiangsu Shuguang Huayang Drilling Tool Co., Ltd. Factory documentation; 4145H, NC46. Original documented batch: 12 pieces, 114.535 m. Includes factory tests and quality checks.
Download PDF27 p. · 0.50 MBJiangsu Shuguang Huayang Drilling Tool Co., Ltd. Factory documentation; 4145H, 6 5/8 FH. Original documented batch: 3 pieces, 28.28 m. Includes factory tests and quality checks.
Download PDF9 p. · 0.40 MBJiangsu Shuguang Huayang Drilling Tool Co., Ltd. Factory documentation; 4145H, 6 5/8 FH. Original documented batch: 6 pieces, 57.442 m. Includes factory tests and quality checks.
Download PDF15 p. · 0.44 MBOutside / inside diameter: 127 × 76.2 mm. Steel: 1340 + 4137H. Connection: NC50.
Download PDF8 p. · 0.46 MBOutside / inside diameter: 247.65 × 76.2 mm. Steel: 4145H. Connection: NC70.
Download PDF6 p. · 0.44 MBThe library includes factory documents from 2016–2017 and additional packages dated 2026. Date of manufacture and current fitness for use are different matters: operational release requires assessment of the actual condition and service history.
ENGINEERING FIRST
Send the well programme, operating loads and required inspection scope.